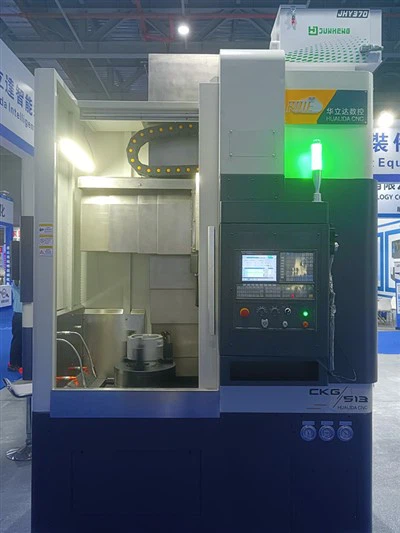
Mechanical structure optimization
Vertical spindle layout
Adopting vertical spindle design, combined with hydrostatic guide technology (radial runout <1μm), combined with large-span columns and rigid beam structure, it effectively suppresses vibration during high-speed cutting, and is suitable for processing parts with large diameter and short length (such as wind turbine hubs and aircraft engine turbine disks).
Dynamic spindle control
Equipped with electronic gearbox (EGB) and constant linear speed cutting function to ensure constant linear speed of the processing surface. The spindle speed can reach 3000r/min, and the speed can be adjusted in real time through the CNC system to adapt to the processing requirements of different materials (such as gray cast iron HT250, high-temperature alloys).
High-speed cutting process
Layered cutting strategy
Roughing stage: Use a φ500mm face milling cutter and adopt stepped layered cutting (cutting depth 4mm, feed 2000mm/min) to quickly remove the excess and reduce clamping deformation3.
Finishing stage: Switch to a smaller diameter tool, reduce the cutting depth (≤0.5mm) and feed rate (finishing feed is usually controlled below 0.1mm/r), and combine constant line speed control to make the surface roughness reach below Ra0.8μm.
Process integration and intelligent control
Compound processing technology
Integrated turning and milling compound functions, through the linkage of the power turret and the C-axis, complex curved surface one-time clamping processing can be achieved (such as the milling of the impeller flow surface and the end face finishing can be completed simultaneously.
Intelligent compensation system
The laser tool setting instrument detects tool wear in real time and automatically compensates for precision deviation;
The thermal elongation compensation system adjusts the Z-axis position through the temperature sensor to control the dimensional error ≤5μm36.
Quality control and stability
Online monitoring
Equipped with pneumatic measuring instruments and vibration sensors to monitor the processing status in real time. For example, when machining cylinder holes, the cylindrical error is dynamically compensated to ≤5μm.
Process stability guarantee
The high-pressure internal cooling system (coolant pressure ≥7MPa) suppresses cutting heat accumulation;
By adjusting the lateral feed rate and tool overhang length, the cutting force fluctuation is controlled within ±8%.